inquiry
Leave Your Message

What Is a Cap Mold and How Does It Work?

A Cap Mold is the precision tool behind the familiar closure on a water bottle, cosmetic container, or medicine package. It shapes molten plastic into a cap with accurate threads, sealing surfaces, tamper-evident bands, and brand details. The process looks simple. It is not.

John Bozzelli, a respected scientific molding educator, describes the broader principle clearly: “A mold is a process, not just a piece of steel.” That idea matters when explaining how a Cap Mold works. Heated polymer enters carefully designed cavities under controlled pressure. The core forms the inner profile, while the cavity creates the outside shape. Cooling channels remove heat before ejector systems release the finished cap.

Small details control the result. A poorly balanced gate can create uneven filling. Weak cooling may cause warping, sticking, or visible sink marks. Thread geometry must also match the container neck with remarkable consistency. One cap may look acceptable, yet leak during testing.

Modern Cap Mold systems often use multi-cavity layouts to produce many closures during one cycle. Hot runners can reduce material waste and improve filling stability. However, these systems demand careful maintenance, temperature control, and process monitoring. Mold performance depends on more than machining accuracy.

This guide examines each stage, from material flow to ejection. It also considers practical design choices, common defects, and maintenance concerns. Some explanations may seem obvious. They are still worth questioning, because small errors often become expensive production problems.
What Is a Cap Mold and How Does It Work?

What Is a Cap Mold?

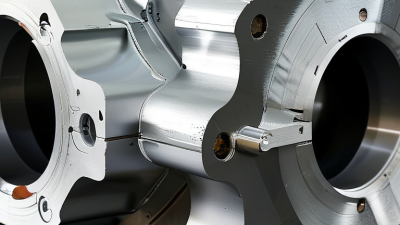
A cap mold is a precision tool that shapes plastic resin into a bottle or container closure. It defines the cap’s outer wall, inner seal, tamper band, and threads. Most molds contain a cavity, core, cooling channels, vents, and an ejection system. Together, these parts control the cap’s dimensions and surface finish. A cap mold is not merely a metal block. It is a repeatable production system.

Plastics Europe reported global plastics production of 400.3 million tonnes in 2022, showing the enormous scale behind everyday plastic components. During injection molding, heated resin enters the cavity under pressure. The material fills the thread profile and then cools against the mold walls. In compression molding, measured plastic doses are compressed between mold surfaces. Cooling channels remove heat, while ejector components release the finished cap. Small venting errors can create burns, short fills, or weak threads. The process sounds simple. It is not always simple.

Tips: Check thread dimensions, cooling balance, and vent depth during mold trials. OECD’s Global Plastics Outlook states that plastic waste reached 353 million tonnes in 2019. That figure supports using lightweight designs without sacrificing sealing performance. Still, lighter is not automatically better. A cap may save material but fail under torque or transport vibration. I would not treat the first trial as final; production evidence should guide the next adjustment.
What Is a Cap Mold and How Does It Work?

A practical overview of cap-mold components, materials, operating steps, and typical production parameters.

Data Dimension Typical Data How It Works or Why It Matters
Definition A precision mold used to form plastic closures such as screw caps, flip-top caps, and dispensing caps. The mold creates the cap’s external profile, internal thread, sealing surface, tamper-evident band, and other functional features.
Main Molding Processes Injection molding and injection-compression molding are common processes for plastic caps. In injection molding, molten polymer is injected into closed cavities. In injection-compression molding, the material is injected and then compressed as the mold closes to improve distribution and reduce stress.
Common Cap Materials Polypropylene (PP) and high-density polyethylene (HDPE) are widely used thermoplastics. PP offers good stiffness and fatigue resistance, while HDPE provides toughness, chemical resistance, and good impact performance.
Mold Structure Typical parts include the cavity, core, neck-ring or thread insert, runner or hot-runner system, cooling channels, guide system, and ejection system. Each section controls a specific portion of the cap geometry and helps maintain repeatable dimensions during high-volume production.
Cavity Count Common production molds may contain 8, 16, 32, 48, 64, or more cavities, depending on machine capacity and required output. More cavities produce more caps per molding cycle but require higher clamping force, balanced filling, and more demanding mold maintenance.
Mold Steel Hardened or pre-hardened tool steels are commonly selected for cavity inserts, cores, and high-wear components. Steel selection affects wear resistance, polishing quality, corrosion resistance, dimensional stability, and expected mold life.
Thread Formation Threads may be formed with unscrewing cores, collapsible cores, or split-core mechanisms. The selected mechanism allows the molded cap to be released without damaging the thread or distorting the closure.
Hot Runner or Cold Runner High-output cap molds often use hot runners; cold runners remain suitable for some lower-volume or simpler designs. Hot runners keep the polymer molten inside the manifold and reduce runner scrap, while cold runners solidify with each cycle and may require trimming or recycling.
Molding Sequence Close mold → inject polymer → pack and hold → cool → open mold → eject caps → repeat. Temperature, pressure, cooling time, and mold-opening speed are adjusted to achieve complete filling, stable dimensions, and clean release.
Typical Cycle Time Approximately 8–20 seconds is common for many injection-molded closures, although some designs run outside this range. Cycle time depends on cap size, wall thickness, resin, mold cooling efficiency, cavity count, and the required dimensional stability.
Cooling System Water channels are usually placed near the cavity and core to remove heat from the molded part. Uniform cooling helps prevent shrinkage differences, warpage, ovality, thread deformation, and inconsistent sealing performance.
Ejection Method Strippers, ejector rings, air assistance, or combinations of these methods are commonly used. The ejection system removes the cap while minimizing marks, deformation, sticking, and damage to the tamper-evident band.
Venting Small vents are positioned near the end of fill and other areas where air may become trapped. Effective venting reduces burn marks, short shots, trapped air, weld-line defects, and variations in surface appearance.
Key Quality Checks Weight, dimensions, thread fit, sealing performance, tamper-band integrity, appearance, and leak resistance. These checks confirm that the cap fits the intended container, protects the contents, and performs consistently during capping and use.
Main Design Objective High repeatability with short cycle times and minimal material waste. A well-designed cap mold balances product performance, production speed, maintenance access, mold longevity, and total manufacturing cost.
Note: Actual mold specifications vary according to cap geometry, resin grade, closure standard, machine capability, production volume, and required quality level.

Main Components and Materials Used in Cap Molds

What Is a Cap Mold and How Does It Work?

A cap mold forms the threads, sealing ring, tamper band, and outer profile of a plastic closure. Molten resin enters the cavity under controlled pressure. The mold then cools, opens, and ejects the finished cap. Small dimensional errors can cause leaks or uneven opening torque.

Its main components include the cavity, core, neck ring, guide pins, cooling channels, runner system, and ejector mechanism. The cavity shapes the outside surface. The core creates the inner thread and sealing geometry. The neck ring supports accurate alignment around the cap opening. Cooling channels remove heat near the thread area, where distortion often appears. Hot-runner systems can reduce material waste, although they increase maintenance demands.

Tool steel remains the standard mold material because it balances hardness, polishability, and wear resistance. Pre-hardened steel suits many medium-volume applications. Hardened tool steel performs better under repeated cycling. Stainless steel helps resist corrosion from moisture or aggressive additives. Copper alloys may improve heat transfer in local inserts.

Material choice is never perfect.

PlasticsEurope reported 413.8 million tonnes of global plastics production in 2023. That scale highlights the value of stable cycle times and long mold life. Industry packaging studies also continue to identify lightweight closures as a major design direction. However, lighter caps can make filling, cooling, and ejection less forgiving. Engineers should verify each design through mold-flow analysis, trial runs, and measured leak testing.

How a Cap Mold Shapes Caps Step by Step

What Is a Cap Mold and How Does It Work?

A cap mold is a precision tool that forms plastic caps through controlled heat, pressure, and cooling. Its cavity creates the outer shape, while the core forms the inner surface and thread. The process begins when plastic pellets enter a heated barrel and become a uniform melt. A screw then pushes the material into the closed mold.

Pressure matters here. Too little pressure can leave short shots or weak threads. Excessive pressure may create flash along the parting line. As the plastic fills the cavity, cooling channels remove heat through carefully placed passages. The mold must cool evenly, or the cap may shrink unevenly and fail to fit its container. Small air vents also help trapped gas escape.

When the plastic reaches a stable temperature, the mold opens. Ejector pins or a stripping system release the cap from the core. Threaded caps often need smooth rotation or controlled stripping to avoid distortion. Operators then inspect dimensions, thread engagement, sealing surfaces, and visible marks. A cap can look acceptable yet leak during testing. That detail is easy to underestimate. Mold maintenance also affects results, since worn surfaces, blocked vents, or poor alignment can gradually reduce quality. In production, minor adjustments are common, and a mold that performs well today may still need redesign after repeated cycles.

Common Cap Molding Methods and Their Differences

A cap mold is a precision tool that shapes plastic into closures for bottles, jars, and containers. It controls the cap’s thread, inner seal, tamper band, and outer texture. During production, heated plastic enters the mold cavity, cools, and releases as a finished cap. A small mismatch matters.

Injection molding is widely used for caps with detailed threads and strong dimensional control. Molten plastic fills each cavity under pressure, then cools around a core. This method supports fast cycle times and complex designs. However, it can create visible gate marks or uneven shrinkage if temperature settings are poorly balanced.

Compression molding uses measured plastic pieces, often called preforms, placed into open cavities. The mold closes and compresses the material into shape. It usually needs less injection pressure and may reduce material stress. It can also provide clean sealing surfaces. Still, accurate dosing is essential. Too much material may create flash around the cap, while too little can weaken the tamper band.

Some manufacturers use injection compression molding, combining injection speed with controlled compression. This approach can improve weight consistency and reduce stress, but the equipment and process control are more demanding. Blow molding is less common for ordinary caps, yet it suits hollow closures or special dispensing structures. In practice, mold selection depends on resin behavior, cap geometry, production volume, and sealing requirements. A design that works well in a laboratory may need adjustment on a high-speed production line. Surface finish, cooling time, and ejection force deserve equal attention.

What Is a Cap Mold and How Does It Work?

Typical cycle time comparison for common cap molding methods. Actual results vary with cap design, resin, mold layout, cooling efficiency, and machine configuration.

Compression molding generally offers shorter cycles and lower material shear because preforms are compressed directly into the cavity. Injection molding is highly flexible for complex geometries but usually requires more cooling time. Injection-compression molding combines injection and compression in one process and can reduce residual stress while maintaining high production efficiency.

Quality Control, Maintenance, and Typical Applications

A cap mold forms the shape, threads, seal, and surface details of a container closure. In production, quality control starts with dimensional checks after molding. Operators measure thread depth, wall thickness, and cap height with calibrated tools. Small defects matter. A slightly uneven thread can cause leakage, poor torque, or difficult opening. Visual checks also reveal flash, sink marks, burn traces, and incomplete filling.

Maintenance is practical, not glamorous. After each production run, technicians remove resin residue from cavities and vents. They inspect ejector pins, sliders, cooling lines, and mold surfaces for wear. Cooling channels deserve special attention because restricted flow can create uneven shrinkage. In my experience, a mold may look clean while deposits remain inside a narrow vent. That assumption is risky. Scheduled lubrication helps, but excessive lubricant can attract dust and contaminate moving areas. Maintenance records should include cycle counts, repairs, measurements, and the person responsible.

Cap molds are widely used for water, beverage, cosmetic, household, and pharmaceutical packaging. Each application may require different thread profiles, sealing features, materials, and cleanliness controls. Food-contact closures need carefully controlled surfaces and suitable production procedures. High-speed lines demand balanced cavities and stable cooling. Testing every setting is not always possible, so sampling plans must be realistic and repeatable. A useful inspection routine may still need revision when field complaints reveal a defect that factory checks missed.